

How designers, fabricators, and buyers can reduce welding distortion through joint design, fit-up, fixtures, sequence, heat control, and inspection matters because custom manufacturing decisions are usually made before the first production problem appears. Buyers, engineers, and quality teams can reduce risk when they review the design, process, inspection plan, and supplier communication together.
This guide focuses on practical checks for Sheet Metal Fabrication projects. It avoids unrealistic promises and instead explains what to confirm, what to ask, and how to keep the project moving with fewer surprises.
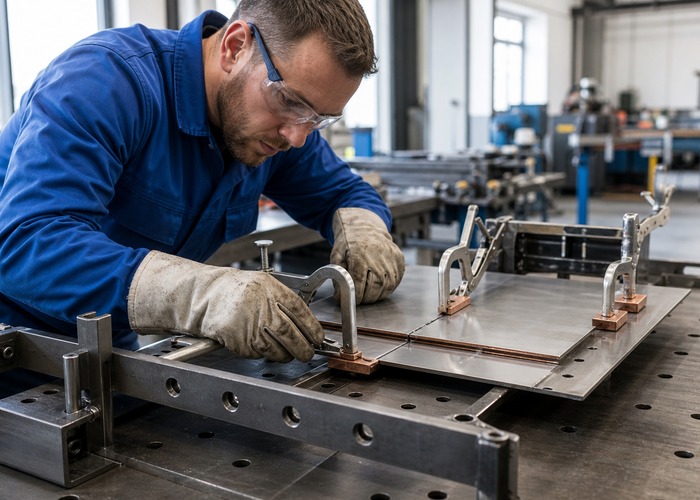
Why thin sheet metal moves during welding
A weld heats a local area rapidly and the metal then contracts as it cools. When that contraction is uneven or restrained, panels can bow, twist, shrink, buckle, or pull out of square even when the cut parts were accurate. The review should connect the part’s real use with material behavior, process limits, inspection method, finishing, packaging, and delivery expectations. When these items are discussed early, the supplier can recommend changes before time and money are committed.
For related service context, review OxRapid Manufacturing while checking how the requirement fits the larger manufacturing plan.
A helpful way to work is to mark each requirement as critical, preferred, or flexible. Critical items protect fit, safety, durability, or customer-facing appearance. Preferred items improve the product but can be adjusted if the supplier explains the tradeoff. Flexible items give the manufacturing team room to simplify tooling, setup, finishing, or inspection.
For related service context, review Die Casting Services while checking how the requirement fits the larger manufacturing plan.
Reduce risk through joint and product design
Shorter welds, balanced joints, bends that add stiffness, accessible seams, realistic tolerances, and well-placed tabs can reduce heat input and movement. Cosmetic panels deserve special attention because even small waves may remain visible after finishing. The review should connect the part’s real use with material behavior, process limits, inspection method, finishing, packaging, and delivery expectations. When these items are discussed early, the supplier can recommend changes before time and money are committed.
For related service context, review 3D Printing Service while checking how the requirement fits the larger manufacturing plan.
A helpful way to work is to mark each requirement as critical, preferred, or flexible. Critical items protect fit, safety, durability, or customer-facing appearance. Preferred items improve the product but can be adjusted if the supplier explains the tradeoff. Flexible items give the manufacturing team room to simplify tooling, setup, finishing, or inspection.
Improve fit-up before the first tack
Gaps, mismatched edges, burrs, contamination, and inconsistent flange positions require extra filler and heat. Clean parts, repeatable cut quality, correct bend dimensions, and controlled joint gaps make the welding process more predictable. The review should connect the part’s real use with material behavior, process limits, inspection method, finishing, packaging, and delivery expectations. When these items are discussed early, the supplier can recommend changes before time and money are committed.
For related service context, review Injection Molding Services while checking how the requirement fits the larger manufacturing plan.
A helpful way to work is to mark each requirement as critical, preferred, or flexible. Critical items protect fit, safety, durability, or customer-facing appearance. Preferred items improve the product but can be adjusted if the supplier explains the tradeoff. Flexible items give the manufacturing team room to simplify tooling, setup, finishing, or inspection.
Use fixtures without creating new problems
Clamps, strongbacks, chill bars, copper backing, locating pins, and rigid tables can hold geometry during welding. Restraint should be applied near the affected area and released in a planned order because excessive restraint can lock in stress. The review should connect the part’s real use with material behavior, process limits, inspection method, finishing, packaging, and delivery expectations. When these items are discussed early, the supplier can recommend changes before time and money are committed.
For related service context, review Mold Making Service while checking how the requirement fits the larger manufacturing plan.
A helpful way to work is to mark each requirement as critical, preferred, or flexible. Critical items protect fit, safety, durability, or customer-facing appearance. Preferred items improve the product but can be adjusted if the supplier explains the tradeoff. Flexible items give the manufacturing team room to simplify tooling, setup, finishing, or inspection.
For related service context, review Sheet Metal Fabrication Services while checking how the requirement fits the larger manufacturing plan.
Plan tack welds and welding sequence
Tack size, spacing, order, and location influence how the assembly moves before final welding. Skip welding, back-step techniques, alternating sides, and working from more rigid areas toward free edges can balance shrinkage. The review should connect the part’s real use with material behavior, process limits, inspection method, finishing, packaging, and delivery expectations. When these items are discussed early, the supplier can recommend changes before time and money are committed.
For related service context, review CNC Machining Services while checking how the requirement fits the larger manufacturing plan.
A helpful way to work is to mark each requirement as critical, preferred, or flexible. Critical items protect fit, safety, durability, or customer-facing appearance. Preferred items improve the product but can be adjusted if the supplier explains the tradeoff. Flexible items give the manufacturing team room to simplify tooling, setup, finishing, or inspection.
Control heat input and weld size
Travel speed, current, voltage, pulse settings, filler size, process choice, and unnecessary overwelding all affect total heat. The smallest weld that meets the engineering requirement is often easier to control than an oversized continuous bead. The review should connect the part’s real use with material behavior, process limits, inspection method, finishing, packaging, and delivery expectations. When these items are discussed early, the supplier can recommend changes before time and money are committed.
For non-commercial background, see OSHA welding safety topic and use it as a reference when discussing safety, terminology, or process risk.
A helpful way to work is to mark each requirement as critical, preferred, or flexible. Critical items protect fit, safety, durability, or customer-facing appearance. Preferred items improve the product but can be adjusted if the supplier explains the tradeoff. Flexible items give the manufacturing team room to simplify tooling, setup, finishing, or inspection.
Measure during fabrication, not only at the end
Check diagonals, flatness, squareness, critical openings, and fixture contact after tack-up and at defined stages. Early measurements allow sequence or restraint adjustments before the assembly becomes too stiff to correct safely. The review should connect the part’s real use with material behavior, process limits, inspection method, finishing, packaging, and delivery expectations. When these items are discussed early, the supplier can recommend changes before time and money are committed.
For non-commercial background, see OSHA welding standard and use it as a reference when discussing safety, terminology, or process risk.
A helpful way to work is to mark each requirement as critical, preferred, or flexible. Critical items protect fit, safety, durability, or customer-facing appearance. Preferred items improve the product but can be adjusted if the supplier explains the tradeoff. Flexible items give the manufacturing team room to simplify tooling, setup, finishing, or inspection.
For non-commercial background, see OSHA personal protective equipment guidance and use it as a reference when discussing safety, terminology, or process risk.
Define an acceptable correction and approval plan
Mechanical straightening or controlled thermal correction may be possible, but correction can create new stress, marks, or dimensional changes. The method, limits, inspection evidence, and cosmetic acceptance should be agreed before rework begins. The review should connect the part’s real use with material behavior, process limits, inspection method, finishing, packaging, and delivery expectations. When these items are discussed early, the supplier can recommend changes before time and money are committed.
For non-commercial background, see NIOSH hierarchy of controls and use it as a reference when discussing safety, terminology, or process risk.
A helpful way to work is to mark each requirement as critical, preferred, or flexible. Critical items protect fit, safety, durability, or customer-facing appearance. Preferred items improve the product but can be adjusted if the supplier explains the tradeoff. Flexible items give the manufacturing team room to simplify tooling, setup, finishing, or inspection.
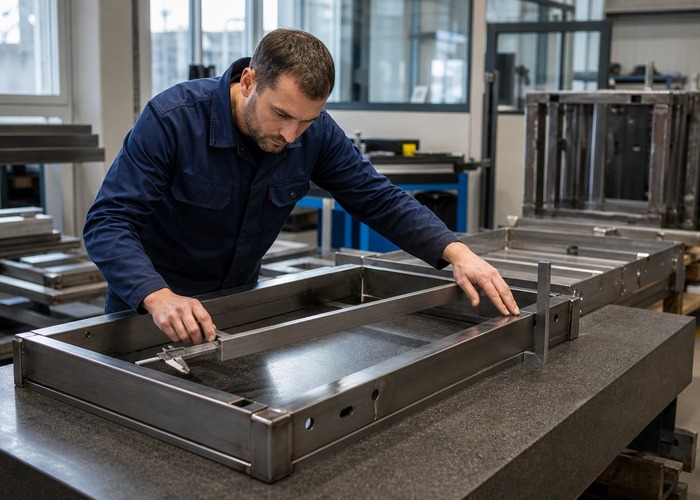
Buyer checklist before approval
Before approving the next step, confirm the latest revision, material, finish, quantity, target use, cosmetic areas, inspection points, packaging notes, and any open risk. For Sheet Metal Fabrication, the most expensive problems often come from small assumptions that were never written down.
For non-commercial background, see welding background and use it as a reference when discussing safety, terminology, or process risk.
Ask for a short written summary of supplier recommendations. The summary should separate changes required for manufacturability from changes that are optional cost or lead-time improvements. This makes it easier for purchasing, engineering, and quality teams to approve decisions without losing context.
Useful approval evidence can include sample photos, inspection results, material confirmation, surface finish notes, packaging photos, and a short explanation of any accepted deviation. The exact evidence should match the project’s risk level. A quick prototype may need only basic confirmation, while a production order should define the important dimensions and appearance limits more clearly.
For non-commercial background, see welding defect background and use it as a reference when discussing safety, terminology, or process risk.
Buyers should also ask how the supplier will communicate problems during production. A good process does not hide issues until final delivery. It defines when the supplier should pause, when a minor adjustment can continue, and who has authority to approve a change. That communication rule protects both schedule and quality.
For non-commercial background, see welding inspection background and use it as a reference when discussing safety, terminology, or process risk.
Common mistakes to avoid
One common mistake is treating a supplier comment as a simple objection rather than a process signal. A comment about access, wall thickness, cooling, support, or maintenance may point to a real production risk. Another mistake is approving a quote without confirming what evidence will be provided after production or trial.
For non-commercial background, see residual stress background and use it as a reference when discussing safety, terminology, or process risk.
It is also risky to discuss finish, packaging, or inspection only after the part is made. Visible surfaces, threaded features, precision areas, and delicate edges need protection throughout production and shipping. Clear expectations help prevent a good part from becoming a rejected part after handling.
A third mistake is comparing quotes only by unit price. A lower price may be reasonable when the design is simple, but it can be risky if it excludes inspection, proper material documentation, finishing control, packaging protection, or enough communication before production. The better comparison is total project reliability, not only the number on the first line of the quote.
For non-commercial background, see heat affected zone background and use it as a reference when discussing safety, terminology, or process risk.
How to communicate changes
When the design changes, state exactly what changed and why. A short revision note helps the supplier focus on the right areas instead of rechecking every assumption. If a change affects a mating component, update both files and explain the assembly impact.
Keep approved decisions in one place: drawing revision, 3D model, material, finish, quantity, inspection points, and accepted supplier suggestions. This simple habit reduces confusion when the project moves from quotation to production.
For non-commercial background, see sheet metal background and use it as a reference when discussing safety, terminology, or process risk.
For repeat orders, keep a record of what worked well and what should be improved next time. That record may include tool notes, fixture notes, packaging changes, inspection findings, or customer feedback after assembly. Reusing that knowledge is one of the simplest ways to make the next order faster and more predictable.
For non-commercial background, see quality control background and use it as a reference when discussing safety, terminology, or process risk.
Quick FAQ
What should I send for a Sheet Metal Fabrication quote? Send a 3D file, controlled drawing, material and finish requirements, quantity, application notes, cosmetic areas, and any mating-part information.
For non-commercial background, see welding distortion control video and use it as a reference when discussing safety, terminology, or process risk.
How early should I ask for design review? Ask before tooling, production setup, or finishing decisions are locked. Early review gives the supplier more room to improve manufacturability without changing the product’s purpose.
What makes a review useful? A useful review identifies critical features, explains tradeoffs, confirms inspection evidence, and records decisions clearly enough that the next production step can proceed without guessing.


