A mold interlock handover should identify the selected alignment components, their installed locations, the manufacturer’s fitting requirements and the condition verified at release. Do not treat every device called a lock as the same component. A precision alignment interlock, a plate-sequencing latch and a transport restraint perform different jobs and need different review criteria.
When planning a mold-making project with FUMING, include the intended alignment strategy and receiving-machine conditions in the design review. This article focuses on the evidence needed to release and maintain precision interlocks. It does not prescribe universal clearances, quantities or installation dimensions.
Separate precision alignment from guidance and sequencing
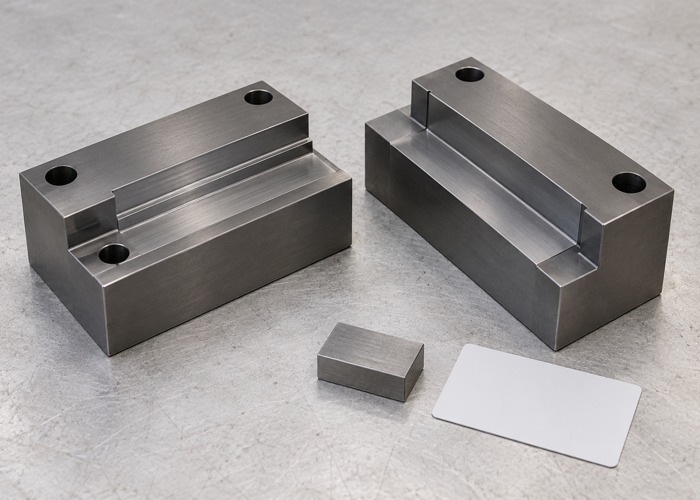
DME’s interlock FAQ explains that interlocks provide more precise parting-line alignment than leader pins. That distinction matters when reviewing a mold: the presence of guide pins does not answer every question about final registry. Identify which components guide the approach and which establish the intended final alignment.
Also identify devices that control plate movement or opening sequence. Their names may include the word lock, but that does not make them substitutes for the alignment elements shown on the design. Use complete manufacturer designations and part numbers in the bill of materials so a purchasing substitution cannot be based on an ambiguous description.
Link the alignment requirement to the features it protects. These may include shutoffs, cavity-to-core relationships or other design-defined interfaces. Record the relevant drawing references rather than claiming that a particular lock automatically eliminates flash or dimensional variation. Part quality still depends on the complete mold and process.
Review the complete system before selecting a component
Consider the mold configuration, moving mass, available installation space and required operating conditions. DME’s mold alignment overview lists part requirements, mold size and type, resin processing temperature and mold life among selection considerations. The useful lesson is to review the application as a system rather than select by the space left in a plate.
Request the current installation information for the exact series and size. Similar-looking parts can have different fitting instructions, engagement characteristics and maintenance requirements. Keep the source document and revision with the design package. A distributor photograph is not enough to establish the dimensions used for machining the pockets.
Document who owns the selection decision and who approves substitutions. If a component becomes unavailable during the build, review the proposed replacement against the application and installation details. Changing a part number after the pockets are machined can affect more than procurement; preserve the engineering assessment and any resulting drawing change.
Check approach and engagement as well as final closure
A component may appear to fit when the mold is fully closed while encountering an undesirable condition during approach. The review should therefore address the path into engagement under the intended setup. Do not infer acceptable operation solely from a static photograph of the closed mold or from a hand-fitted loose component.
The DME mold interlock product sheet discusses alignment influences associated with the movable platen and guide components. For the project record, identify the machine and mold conditions represented by the trial. A bench check and an installed-machine check should be labeled as different evidence.
Keep observations specific: location, stage of movement, contact evidence and associated conditions. If an unexpected mark or resistance appears, stop the evaluation under the approved procedure and investigate. Do not recommend grinding, forcing or increasing closing force as a generic remedy. The responsible toolmaker must determine the cause and an approved correction.
Preserve fitting evidence without inventing a universal target
| Evidence item | What to record | Why it matters |
|---|---|---|
| Component identity | Series, size, part numbers and location | Connects installed parts to approved selection |
| Pocket and mounting references | Controlled drawing and fitting instruction revision | Prevents comparison with the wrong requirements |
| Engagement review | Condition and sequence evaluated | Distinguishes approach behavior from final closure |
| Contact observations | Location, method and approved interpretation | Avoids treating any visible mark as acceptable |
| Trial configuration | Machine, relevant temperature state and mold revision | Defines the scope of the evidence |
| Disposition | Accepted state or approved corrective action | Makes unresolved conditions visible at handover |
If a contact-marking method is used, follow the specified method and interpretation. A photograph of transfer marks should be accompanied by the surface identity and test conditions. There is no single contact percentage that this guide can assign to every interlock design. The selected manufacturer’s instructions and approved design govern acceptance.
Record any fitting work that changes an installed component or mounting surface. Update the as-built record where required. A spare purchased under the original catalog number may need additional review if the working installation contains undocumented modifications. Keeping those changes visible makes future maintenance more predictable.
Use trial results with appropriate limits
A successful trial provides evidence for the configuration that was actually tested. Record relevant operating conditions and any changes made during the trial. If an interlock was replaced or adjusted between sample sets, identify which configuration produced the accepted parts. Do not combine observations from different arrangements into one unexplained approval.
Review the alignment evidence alongside the part measurements and observed mold behavior. A passing sample dimension does not by itself prove that every alignment component is installed correctly. Conversely, a visible mark does not identify the cause of a dimensional problem without further investigation. Keep mechanical observations and sample results connected but distinct.
The quality assurance handover should include unresolved items and the person responsible for disposition. Where the receiving site uses another machine or operating arrangement, identify what must be reconfirmed. The broader mold transfer checklist helps organize those receiving-site responsibilities.
Make maintenance records component-specific
List the selected manufacturer’s inspection and service requirements, using the actual component identification. Record the approved lubrication instructions where applicable instead of writing a generic instruction to grease every lock. Different designs may have different requirements; an informal practice carried over from another mold is not enough.
Give maintenance personnel a location map and a way to record wear or damage consistently. Photographs should show the same identified surfaces where comparison is intended. Document the operating context and prior interventions when a change is found. A dated image without a component identity is difficult to use after several similar molds enter service.
Plan spare components and replacement verification before a failure occurs. State whether the replacement requires fitting, paired-component review or another check under the selected instructions. Do not assume that replacing one visibly damaged item restores the whole alignment system. Inspect related features according to the approved investigation scope.
Include alignment evidence in the release package
The receiving team should obtain the final bill of materials, location drawing, installation references, relevant trial observations and maintenance requirements. Keep the package tied to the released mold revision. If a temporary trial component remains installed, label its disposition clearly rather than allowing it to become an undocumented production default.
Coordinate that package with the injection molding setup requirements. Confirm who supplies the receiving-machine information and who signs off any required reconfirmation. Good documentation makes a later comparison possible without promising that one component will solve every alignment issue.
Questions buyers often ask
Are leader pins and precision interlocks interchangeable?
No. Their roles in the selected design must be identified separately. Follow the approved alignment strategy and the component manufacturer’s requirements.
Does a closed-mold fit prove acceptable engagement?
No. The relevant approach and operating conditions also need review. State exactly what the check covered and what remains to be verified.
What belongs in the quotation request?
Provide the mold configuration, alignment requirements, receiving-machine information and required release evidence. Ask FUMING to review the tooling scope so that component selection, fitting and handover records are included from the start.