

Hardware kills companies slowly. A promising prototype sits in a lab while competitors ship, investors grow impatient, and market windows close. The gap between a functional proof-of-concept and a production-ready enclosure has historically been one of the most dangerous stretches in any hardware startup’s journey — expensive, unpredictable, and brutally unforgiving.
“The shift toward ‘On-Demand Manufacturing’ is no longer a luxury but a necessity for hardware startups looking to bridge the gap between a functional prototype and a scalable product.” — MIT Technology Review (Insights)
That observation cuts to the heart of a structural problem. Traditional manufacturing pipelines were designed for certainty: large batch sizes, fixed tooling investments, and lead times measured in months. Modern hardware development demands the opposite. Time-to-market has become the primary KPI that separates funded teams from failed ones, and the pressure is only intensifying. The global sheet metal fabrication market is projected to reach $110.1 billion by 2030, growing at a 4.1% CAGR — a signal that industrial demand for precise, repeatable enclosures isn’t slowing down.
On-demand manufacturing directly addresses R&D friction by compressing iteration cycles. Instead of committing to expensive tooling before a design is validated, engineering teams can use custom sheet metal fabrication services to produce bridge units, pilot runs, and production-intent parts on parallel timelines. The result is fewer redesign surprises and faster path-to-revenue.
Speed matters most when it doesn’t compromise structural integrity or dimensional accuracy. That’s precisely where material selection becomes the engineering discipline that determines whether a fast-moving hardware program actually scales — or simply ships fast and fails in the field.
Material Selection: The Engineering Foundation of Precision Enclosures
Speed only matters if the part you’re shipping actually works. Once you’ve committed to moving fast, the next decision that defines success or failure is material selection. Get it right, and you have a product that survives real-world conditions, passes certification, and ships on time. Get it wrong, and you’re back at square one — reworking tooling, chasing approvals, and burning runway.
According to Thomasnet industrial sourcing data, Aluminum 5052 and Stainless Steel 304 remain the most sought-after materials, accounting for over 50% of all precision enclosure projects. That statistic isn’t arbitrary — it reflects decades of engineering consensus around what works at scale.
| Material | Key Property | Best Use Case |
|---|---|---|
| Aluminum 5052 | High formability, corrosion resistance | Electronics enclosures, consumer hardware |
| Stainless Steel 304 | Strength, oxidation resistance | Industrial panels, food processing |
| Stainless Steel 316 | Superior chloride resistance | Marine, pharmaceutical, medical |
| Titanium Grade 5 | Exceptional strength-to-weight ratio | Aerospace, defense hardware |
Aluminum 5052: The Workhorse Alloy
For electronics enclosures, Aluminum 5052 is the default choice for good reason. It offers excellent formability, welds cleanly, and resists corrosion without demanding complex surface treatments. Its relatively low density keeps assembled unit weights manageable — critical when thermal management and portability both matter. In practice, 5052 also accepts anodizing and powder coating predictably, which compresses secondary finishing timelines.

Stainless Steel 304 vs. 316: Reading the Environment
Stainless Steel 304 handles most industrial environments with ease. However, when chloride exposure enters the picture — saltwater, sterilization chemicals, or high-humidity cleanrooms — Grade 316 becomes mandatory. This distinction matters enormously in sheet metal fabrication for medical equipment, where regulatory compliance and patient safety make material substitutions non-negotiable. The cost delta between 304 and 316 is real, but it’s rarely the largest line item when weighed against the cost of a failed audit.
Specialty Alloys: Aerospace and Beyond
When mass is the enemy, Titanium Grade 5 (Ti-6Al-4V) delivers strength-to-weight ratios that aluminum and steel simply can’t match. Aerospace and defense programs routinely specify it for structural enclosures where every gram is accountable. The trade-off is longer lead times and tighter machining tolerances.
Material choice also cascades directly into how a part is designed for production. The alloy you specify today shapes every downstream decision — and that’s precisely where design for manufacturability becomes the next critical lever to pull.
DFM: The Difference Between a Part and a Product
Getting material selection right — as covered in the previous section — is only half the engineering equation. The other half is designing that material to be manufactured efficiently. That’s where Design for Manufacturing (DFM) transforms a technically sound prototype into a scalable product. Without it, companies burn budget on rework, custom tooling, and scrap rates that quietly erode margins before a single unit ships.
DFM isn’t a checklist — it’s a discipline that forces engineers to treat the factory floor as a design constraint, not an afterthought.
The payoff is measurable. According to the American Society of Mechanical Engineers, applying DFM principles in sheet metal fabrication can reduce material waste by up to 30% while significantly compressing production timelines. That’s not an incremental improvement — it’s a structural cost advantage.
Applying DFM to sheet metal can reduce material waste by up to 30%, directly improving margins and accelerating production timelines. — ASME
The Golden Rules of Sheet Metal DFM
Whether you’re working from a sheet metal material selection guide or starting fresh from a CAD file, these principles apply across virtually every enclosure design:
- Standardize bend radii. Custom bend tooling adds lead time and cost. Keeping bend radii consistent — ideally equal to the material thickness — allows fabricators to use standard press brake tooling without setup delays.
- Follow the 2x Thickness rule for holes. Hole diameters should be at least twice the material thickness, and positioned no closer than twice the thickness from any edge. Violating this causes deformation, cracking, and failed tolerances — problems that surface late and cost disproportionately to fix.
- Maintain uniform wall thickness. Inconsistent wall thickness creates stress concentrations during bending and welding. Uniformity isn’t just aesthetic — it’s a prerequisite for structural stability under real operating loads.
- Design for standard hardware. Where possible, design mounting features, slots, and fastener holes around off-the-shelf hardware. Custom fasteners create supply chain dependencies that slow both production and maintenance.
On the other hand, DFM does require upfront investment in design reviews. Skipping that step to save time almost always creates larger delays downstream — a pattern consistently observed when scaling hardware from pilot to production runs.
These principles apply broadly across enclosure types, but the stakes escalate considerably in regulated industries where manufacturing tolerances intersect with patient safety and structural certification — a reality explored in the next section.
Critical Applications: Sheet Metal in the Medical and Aerospace Sectors
Material choices and DFM principles don’t exist in a vacuum — they get put to the test hardest in industries where failure isn’t an option. Medical equipment and aerospace hardware represent two of the most demanding environments for precision sheet metal, and understanding what each sector requires reveals why design decisions made early in the process have consequences that compound over time.
Medical Equipment: Cleanability, Biocompatibility, and EMI Shielding
In medical environments, an enclosure does far more than house components. It has to survive repeated chemical sterilization without degrading, resist corrosion from cleaning agents, and — critically — not introduce contaminants into sterile fields. This is why 316L stainless steel is a common choice for medical-grade enclosures: its low carbon content improves corrosion resistance, and its surface can be electropolished to a finish that prevents bacterial adhesion.
EMI shielding is another non-negotiable. Sensitive diagnostic equipment operates in electrically noisy hospital environments, and poorly designed enclosures can compromise signal integrity. Precision-formed sheet metal, with tight seam tolerances and conductive gasket integration, provides a reliable Faraday cage effect that protects internal electronics.
Aerospace: Lightweighting Without Sacrificing Structural Rigidity
Aerospace applications demand a different kind of discipline. Every gram removed from a component is a gram that improves fuel efficiency or payload capacity, yet structural integrity cannot be compromised under thermal cycling, vibration, or pressure differentials.
Aluminum alloys — particularly 6061-T6 — strike this balance effectively, offering a strength-to-weight ratio that makes them a staple in airframe and avionics enclosures. According to Grand View Research, precision components in automotive and aerospace are critical for maintaining competitive development cycles in high-precision manufacturing. A well-executed bend radius and consistent wall thickness matter enormously here; inconsistencies that would be acceptable in commercial-grade work become structural liabilities at altitude.
Why Enclosure Design Dictates Component Longevity
There’s a principle that holds true across both sectors: the enclosure is not passive packaging — it’s an active engineering decision. Internal components — circuit boards, sensors, actuators — perform to their rated specifications only when thermal dissipation, vibration dampening, and moisture ingress are managed at the enclosure level.
Example scenario: An avionics unit designed with insufficient panel rigidity develops micro-vibrations during flight. Over hundreds of operating hours, solder joints fatigue and fail — not because of a component defect, but because the enclosure design didn’t account for resonance frequencies. This same logic applies to medical imaging equipment subjected to daily transport across hospital floors.
Sheet metal fabrication quality control in these regulated industries isn’t just best practice — it’s a regulatory requirement. ISO-certified manufacturing processes ensure dimensional consistency, material traceability, and documented inspection records that hold up to FDA or FAA scrutiny. That rigor doesn’t stop at the metal; it extends to integrated components, which is why teams often coordinate enclosure design alongside decisions about high-volume component production to ensure everything fits together under production conditions.
The stakes in these sectors make one thing clear: getting quality right on the first production run isn’t just efficient — it’s essential. That’s exactly what a structured quality control process is designed to guarantee, which we’ll examine in detail next.
Quality Control: Beyond the Visual Inspection
Precision fabrication and smart Design for Manufacturing DFM decisions only deliver value if quality control catches every deviation before parts reach assembly. In high-stakes industrial hardware, a rigorous QC process isn’t a final checkpoint — it’s a continuous thread woven through every production stage.
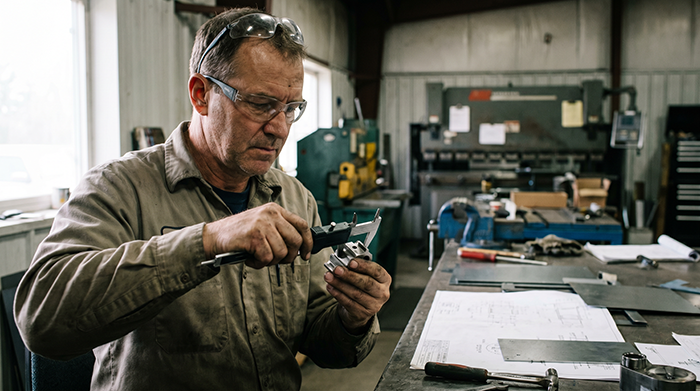
First Article Inspection (FAI) is where that thread begins. Before a full batch run proceeds, FAI validates that the first produced part meets every dimensional, material, and finish requirement in the specification. It’s the mechanism that prevents a small tolerance drift from multiplying across hundreds of components. In volume production, catching a 0.3mm deviation at part one costs far less than discovering it at part five hundred.
Dimensional accuracy is typically governed by ISO 2768, the international standard for general tolerances covering linear dimensions, angles, and form. A fabrication partner who references ISO 2768 explicitly — and documents their measurement results — signals that their process is controlled, not just estimated.
Material traceability is equally non-negotiable. Every sheet of metal used in a certified production run should carry documentation linking it to its mill source, chemical composition, and mechanical properties. Without that paper trail, downstream audits — especially in the medical and aerospace sectors covered earlier — become a serious liability.
According to MIT Technology Review, ISO-certified quality control is a primary driver in reducing time-to-market for industrial tech companies. That connection between certification rigor and speed is counterintuitive but real: consistency eliminates rework cycles.
Surface finish consistency across batch runs — Ra values, coating uniformity, edge deburring — closes the loop. Visual inspection alone doesn’t capture it.
What to Ask Your Fabrication Partner About QC
- ✅ Do you perform First Article Inspection (FAI) on new part runs?
- ✅ What tolerance standard do you apply — ISO 2768 fine or medium?
- ✅ Can you provide material certifications and mill traceability documentation?
- ✅ How do you measure and record surface finish consistency across batches?
- ✅ Are your QC processes backed by ISO certification?
A partner who answers these questions with documentation — not just assurances — is the kind of partner capable of supporting you beyond a prototype. That distinction becomes the foundation of any serious long-term manufacturing relationship.
Key Takeaways
- ✅ Do you perform First Article Inspection (FAI) on new part runs?
- ✅ What tolerance standard do you apply — ISO 2768 fine or medium?
- ✅ Can you provide material certifications and mill traceability documentation?
- ✅ How do you measure and record surface finish consistency across batches?
- ✅ Are your QC processes backed by ISO certification?
Conclusion: Choosing a Partner for the Long Haul
Scaling industrial hardware from prototype to production isn’t a single leap — it’s a series of deliberate decisions that compound over time. Throughout this article, three pillars have emerged as non-negotiable: material selection, Design for Manufacturing (DFM), and rigorous quality control. Get all three right, and precision sheet metal becomes a genuine competitive advantage. Miss any one of them, and costs spiral, timelines slip, and production quality becomes unpredictable.
The bridge between prototyping and mass production is where most hardware programs either gain momentum or stall out. As research into hardware scaling challenges confirms, the jump from a working prototype to a manufacturable, scalable product involves friction points that engineering decisions made early can either eliminate or amplify. Choosing the right fabrication partner at that inflection point isn’t a procurement detail — it’s a strategic call.
Precision manufacturing demands more than capability. It demands speed, consistency, and accountability at every stage of the process.
This is where on-demand manufacturing through OxRapidMFG changes the equation. With 1-day lead times and access to 700+ manufacturing centers, OxRapidMFG compresses the feedback loop between design intent and physical output. Whether you’re refining tolerances for a medical enclosure or validating geometry for an aerospace bracket, faster iteration means fewer costly surprises downstream. For teams exploring complementary processes, OxRapidMFG’s custom molding capabilities also support broader manufacturing programs that go beyond sheet metal alone.
Your Next Step
The fastest way to understand what your design costs — and where it can be optimized — is to get a real quote against a real file.
Upload your CAD file today and receive an instant quote from OxRapidMFG. No guesswork. No delays. Just actionable data that moves your project forward.


